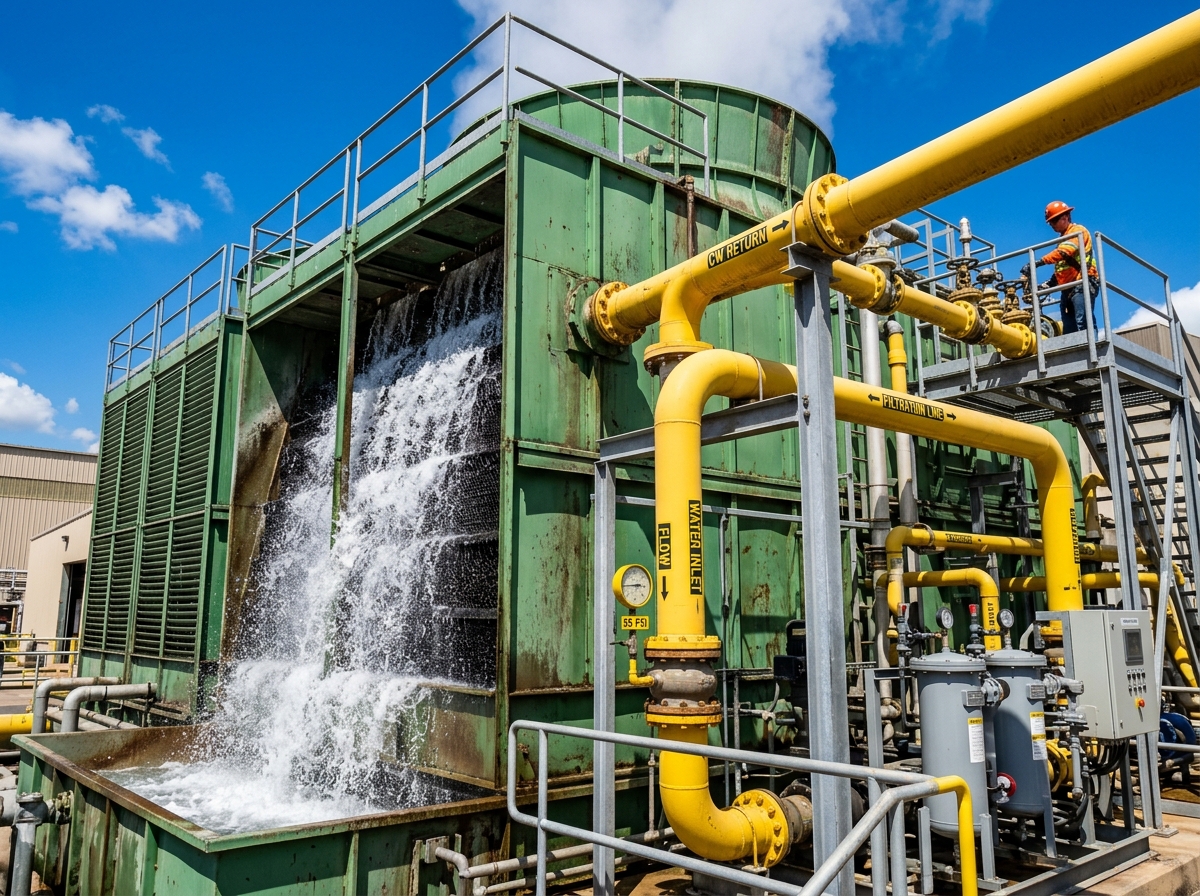
Cooling Systems
Cooling Tower Treatment
Controls high alkalinity, carbonate scale, and microbiological slime to maintain peak chiller heat exchange and reduce drift loss.
Protect heat transfer, eliminate scaling, prevent severe corrosion, and cut boiler & chiller power consumption by up to 18%. Backed by deep chemistry knowledge and end-to-end technical support.
We manufacture targeted formulations to eliminate scale, inhibit corrosion, prevent biological fouling, and control dissolved oxygen across critical thermal and membrane utilities.
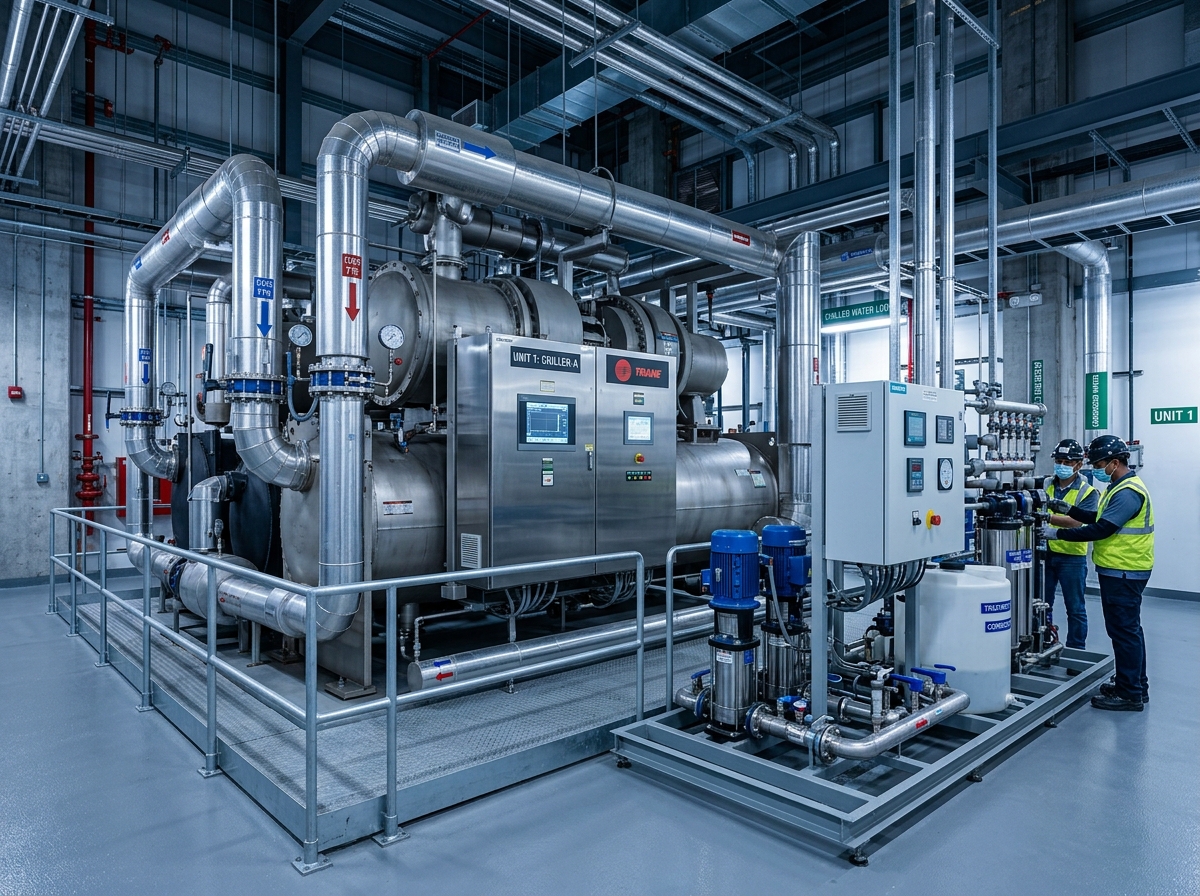
Cooling Systems
Controls high alkalinity, carbonate scale, and microbiological slime to maintain peak chiller heat exchange and reduce drift loss.
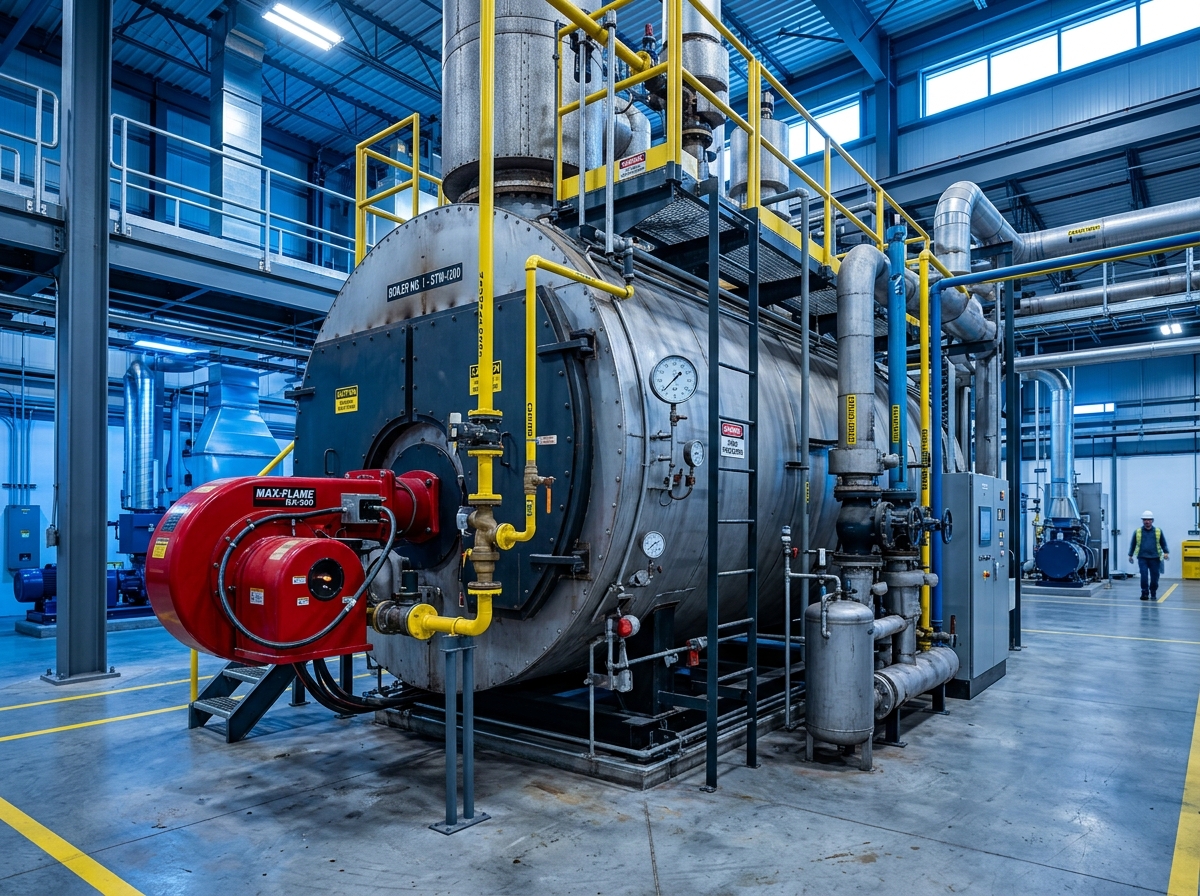
Steam Systems
Removes dissolved oxygen, prevents caustic embrittlement and scale deposits, ensuring high thermal efficiency and clean steam.
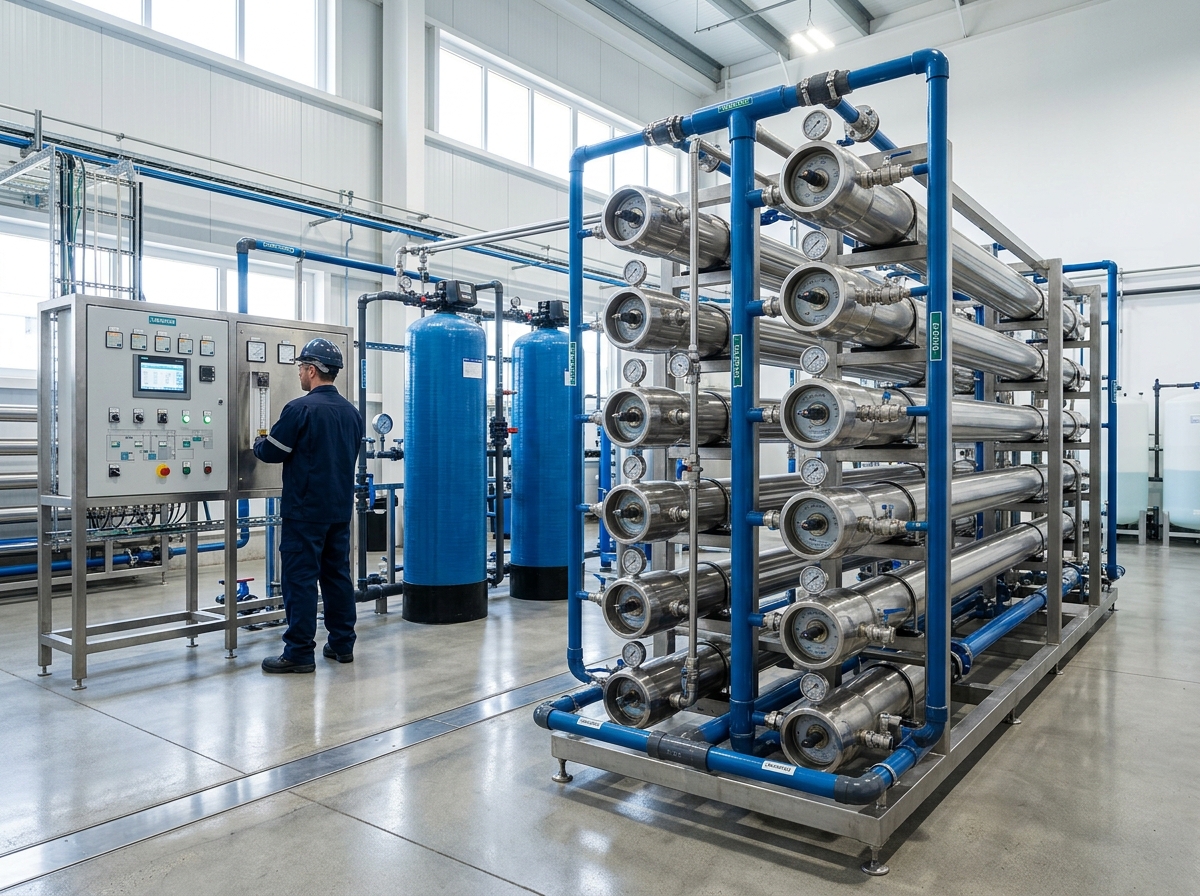
Membrane Systems
High-recovery antiscalant preventing silica, gypsum, and calcium carbonate clogging. Extends membrane life up to 8+ years.
Closed Loop HVAC
Nitrite-based closed-loop corrosion inhibitor protecting multi-metal assemblies (Copper, Brass, Carbon Steel, Stainless Steel).
Untreated industrial water creates rapid scale formation, microbial biofilm, and acid corrosion. See the measured difference DSL chemistry makes to your equipment and balance sheet.
Heavy operational degradation & premature capital breakdown
Peak thermal efficiency, maximum recovery & 3x longer plant life
| Equipment Component | Lifespan Without Proper Treatment | Lifespan With DSL Treatment Program | Expected Improvement |
|---|---|---|---|
| Condenser Tubes (Copper / SS) | 3 โ 7 Years | 10 โ 15+ Years | +200% Lifespan |
| Boiler Tubes (Carbon Steel) | 3 โ 5 Years | 10 โ 15+ Years | +250% Lifespan |
| Cooling Tower Fill (PVC / PP) | 2 โ 5 Years | 5 โ 10 Years | Double Durability |
| Boiler Drum & Headers | 10 โ 15 Years | 20+ Years | Zero Embrittlement |
| RO Plant Membranes | 2 โ 4 Years | 5 โ 8+ Years | Higher Permeate Recovery |
| Chilled Water Piping & Tanks | 5 โ 10 Years | 15 โ 25 Years | Minimal Pitting & Sludge |
Estimate your plant's energy reduction, equipment life extension, and projected chemical requirements in seconds based on your plant capacity.
Based on typical industry operating conditions. Actual savings may vary depending on water quality, operating practices, energy costs and system design.
Chemical supply is only half the battle. We provide continuous technical monitoring, on-site sampling, lab analysis reports, and spare parts.
From sterile pharmaceutical manufacturing to heavy textiles and petrochemical units, our chemicals deliver clean water and reliable heat transfer.
High purity utility water chemistry, strict regulatory compliance, cooling tower, boiler and RO chemicals.
Aggressive cooling systems, high-stress heat exchangers, heavy scale and corrosion protection.
High steam load boilers, process water softness, effluent reuse, and non-corrosive steam lines.
Cooling towers for induction furnaces, metal processing machinery, and chiller system preservation.
Safe, hygienic microbial control, scale-free pasteurizers, and reliable steam for processing.
Central HVAC chiller plants, cooling towers in commercial complexes, hospitals, and luxury hotels.
We combine profound academic chemistry foundations with hands-on industrial plant fieldwork.
Founded by chemistry educators with deep molecular understanding of scale crystallization and corrosion mechanisms.
Comprehensive on-site and laboratory water testing ensuring chemical dosing is backed by hard empirical data.
We tailor antiscalant, biocide, and corrosion inhibitor ratios specifically to your raw feed water quality.
Direct manufacturer pricing with no middlemen, lowering total cost of ownership by up to 25%.
Request a free on-site water quality analysis and get tailored chemical dosing recommendations from Sachin Patel and the DSL Chemicals engineering team.